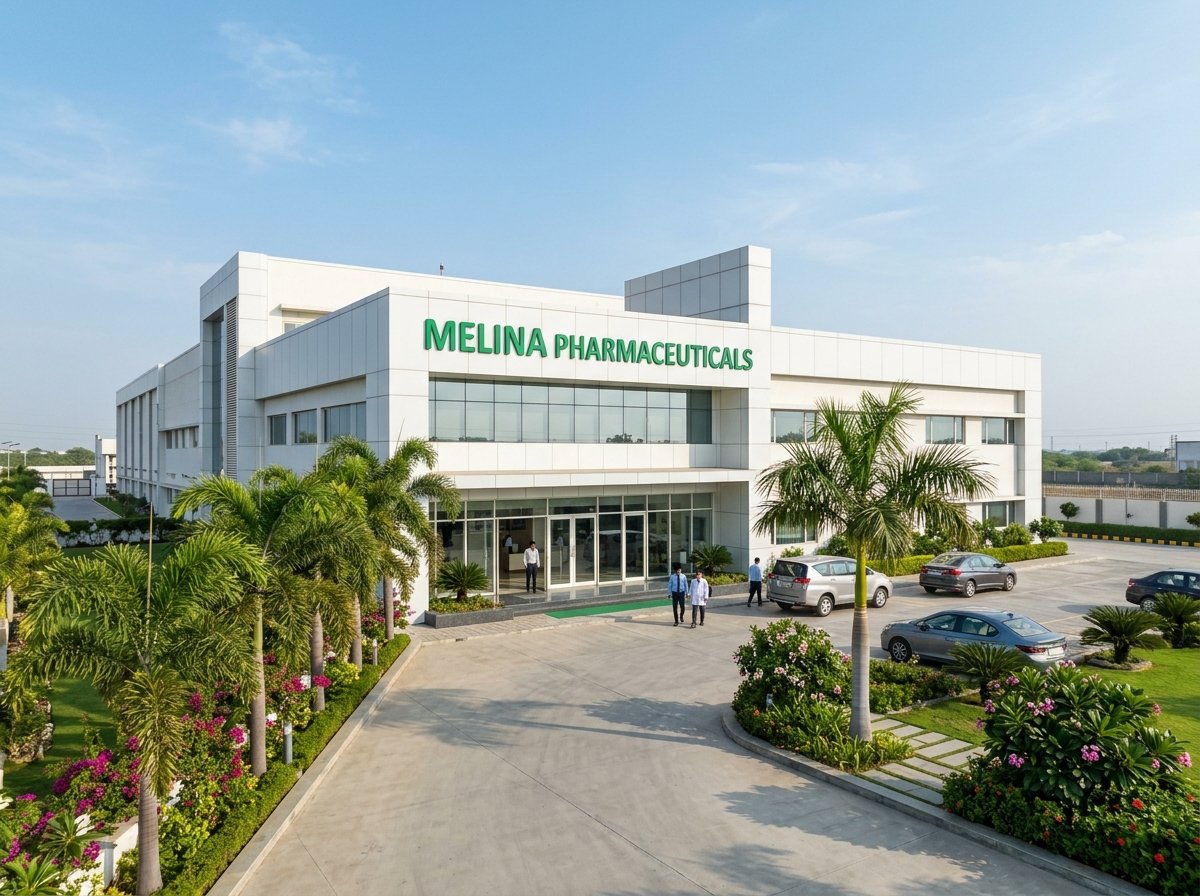
Engineered Cleanroom Facilities & Campus Architecture
Located in Nanguneri, Tirunelveli, Melina Pharmaceuticals operates a purpose-built pharmaceutical complex designed strictly under AYUSH GMP and ISO 9001:2015 cleanroom standards for authentic Siddha formulations.
Unidirectional Linear Workflow Architecture
Our plant layout strictly implements unidirectional movement for raw botanicals, personnel, packaging materials, and finished medicines. Airlocks, differential pressure cascades, and pass-boxes prevent any cross-contamination between processing wings.
Every section is partitioned with pharmaceutical-grade modular sandwich panels, flush double-glazed view windows, and seamless coved epoxy flooring that withstands aggressive sanitation protocols.
No Backtracking
Raw herb intake to quarantine to warehouse in an uninterrupted linear chain.
Airlock Enclosures
Multi-tier gowning airlocks with interlocking doors for all cleanroom entries.
Critical Plant Utilities
Advanced automated auxiliary utilities ensure uncompromised pharmaceutical precision across every batch.
Pharmacopoeia RO Water
Multi-stage Reverse Osmosis and demineralization loop with SS-316L continuous sanitary recirculation piping at 65°C.
Conductivity < 1.3 μS/cmClass 100K HVAC Loop
Dedicated Air Handling Units (AHU) with terminal HEPA 0.3μ filters providing 20 to 25 air changes per hour under positive pressure.
99.97% HEPA EfficiencyClimate Herb Warehousing
Dehumidified botanical storage keeping herbs at 20–25°C and <45% RH to prevent microbial degradation and oxidation of active volatiles.
Continuous RH LoggingZero Liquid Discharge
On-site biological and membrane effluent treatment plant (ETP) ensuring zero wastewater leaves the complex, protecting Tirunelveli's water table.
100% Water RecycledFacility Cleanroom Zoning Matrix
Strict environmental containment architecture segregating processing stages to eliminate environmental contaminants.
Formulation Cleanrooms
Primary liquid filling, rotary tablet compression, and sterile blister packaging suites.
- ISO Class 8 (100K) positive pressure
- HEPA 0.3μ terminal filtration
Botanical Pulverization
High-speed micro-pulverizing pin mills, vibro-sifters, and cyclone separation units.
- Negative pressure dust capture
- Airborne powder isolation
Aqueous Steam Extractors
Steam-jacketed stainless steel vessels for decoctions, Thailams, and herbal Lehyams.
- SS-316L pharmaceutical contact
- Automated steam thermal loggers
Controlled Botanical Storage
Quarantine bays and temperature/humidity-regulated finished formulation warehouse.
- Temperature 20°C–25°C • <45% RH
- ERP palletized digital tracking
Partner With an Audited Siddha Manufacturer
We welcome authorized healthcare institutions, Siddha clinics, distributors, and contract manufacturing partners for physical facility inspections and regulatory audits.